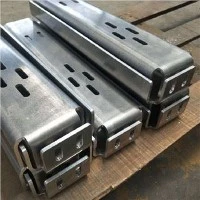
Az a döntés, hogy hengeralakítást vagy présfékezést válasszunk, azon múlik, hogy milyen gyártási megoldással lehetne elérni a kívánt minőséget a legalacsonyabb gyártási költség mellett, és számos tényezőt figyelembe kell venni. Megosztjuk veled gondolatainkat az előnyeiről és hátrányairólfémformázás solutions and hope our experience will help you to make the right decision for your next project.

Először is nézzük meg, mi az a présfékezés. A présfékezés, más néven fékalakítás vagy préshajlítás, egy fémdeformációs folyamat, amely egy fémlemezt vagy fémlemezt egy tengely mentén igazít. Ezt úgy érik el, hogy egy gépi présszerszámot (nyomófék) használnak, hogy a fémdarabot a lyukasztó és a szerszámkészlet közé szorítsák az előre meghatározott hajlítási szöghez. A kiváló minőségű-présfékezés érdekében egy gyakorlott kezelő módszeresen végigmegy egy lépéssorozaton, amely magában foglalja az ellenőrzést, a beállítást és az újraellenőrzést, hogy megbizonyosodjon arról, hogy minden megfelelően van beállítva a lehető legideálisabb kanyarhoz. Kérjük, mindig ne feledje, hogy a pontos hajlítások eléréséhez három kritikus összetevőt kell figyelembe venni: a féknyomó, a szerszámok (lyukasztás és a matrica) és maga az anyag.
Az anyag esetében néhány szempontot kell figyelembe venni:
√ Hardness, which is how resistant the metal is to be penetrated, and it's normally measured by the Rockwell scale.
√ Springback effect, normally operators will overbend an angle because the material returns back towards its original shape after bending.
√ A hozamerősség, amely döntő tényező abban, hogy mekkora igénybevételt tud elviselni alakja megváltoztatásához.
√ Ductility, it often means elongation, and it measures the capability of the metal to be stretched without breaking.
√ Vastagság, a fémvastagság másképp reagál a hajlítási nyomásra.
√ Szemcse irány.
A présfékező gép esetében a tapasztalt kezelő a következő szempontokat is figyelembe veszi.
√ Tonnage, calculate the correct tonnage needed for your bending specification. the bend you are trying to achieve, the length and thickness of the
workpiece, the inside radius of the formed part, the V-die opening, and the minimum amount of flange on the finished part.
√ Bend sequence, make sure that the bending sequence gives you the best quality with minimum defect ratio.
√ Bending solution, you need to know which one to choose from air bending, bottoming, or coining, determine the most suitable bending method according
to your client's requirement.
√ Y-axis, aiming the exact same spot with each cycle.
√ Calibration, just like calibrating your inspection tools, and you need to verify that your brake is calibrated properly on the regular basis. If there is big project
that requires high accuracy, you need to recalibrate it even if you have just done it not too long ago.
A présfékezés utolsó fontos eleme a szerszámozás, és kezelőjének a következő tényezőket kell figyelembe vennie:
√ Seating, the operator needs to make sure that the press forming tooling is properly to positioned to ensure a correct bend. Usually, hydraulic clamping is
recommended.
√ Positioning, in practical most bending is performed in the center of the press brake ram, but you might consider setting up several different sets of tooling at
once for stage bending if that does not impact upon your bending result in a negative way.
√ Tooling selection, the operator needs to make sure that the upper tooling and bottom dies needs to handle the tonnage you've calculated for the
operation.
√ Kompatibilitás, ha rendelkezik CNC présfékkel, mindig ne felejtse el beadni a lyukasztó és a szerszám pontos méreteit a következetes programozás érdekében
operation.
A fékalakítás az egyik legrégebbi mechanikai alakváltozási megoldás, és nagyon sokféle formát képes előállítani, és a présfékezés előnyei:
√ Ideal for low- to medium-volume orders, especially for smaller and shorter components.
√ Relatively low tooling cost compared with roll forming.
√ Ideal for high-mix, low-volume projects.
√ Simple to set up and operate than roll forming.
√ Cost-effective, and it is capable of bending metal at almost any orientation or position; its
limitation being that there must be ample room for the metal being bent to fit inside and around
the press brake.
√ Capability of forming wide different shapes.
√ Short cycle time.
√ Suitable for wide different metal material like aluminum, stainless steel, copper, CRC, HRC
√ Cost of press braking machine is usually lower than roll forming machine.
√ Requires less space than roll forming machine.

A préshajlítás hátrányai a következők:
√ Limit to the length of the bend, and usually the maximum length will be under 6,000mm. TLeggyakoribb hossza 3,000mm alatti
√ Not suitable for high volume, unless robotic press bending equipment is invested. An automated press brake bending cell like the one we described is quite
expensive. Plus, it needs engineering support to program new projects. Offline programming is feasible, but robot programs usually need some on-machine
touch up.
√ Can't produce complex shapes because the brake dies aren't made for complex forming.
√ Can't make long workpiece, which is longer than 6,000mm.
√ Press braking requires separate fabrication processes for punching, notching, or perforating, which requires time, labor, and expense.
In short, the press brake is flexible and very versatile, and it has a limit to the sheet size and length of bending. In contrast, roll forming works on long lengths of coiled material, and the formed pieces then need be cut into desired length. With above explained pros and cons about press braking, you might have a clearer idea about this metal forming process. Now, let's take a look at the process of roll forming, and what's the advantage and disadvantages of roll forming?
A hengeralakítás egy megbízható fémalakító megoldás, amely folyamatos hajlítási műveletet alkalmaz, ahol hosszú fémszalagokat, jellemzően tekercselt acélt vezetnek át egymás utáni hengersorokon szobahőmérsékleten. A hengeralakítás sebessége néhány métertől több mint száz méter/percig változik, így valóban nagyon magas gyártási hatékonyság érhető el.
A hengeralakítás előnyei
√ Multi production solution, and it incorporates secondary operations such as punching and notching in-line, the ability to form complex shapes that can't be
press bent.,
√ Produce extra-long metal profiles that can't be produced by brake press.
√ Capable of producing different lengths
√ High efficiency, it can produce tight tolerance with relatively high speed.
√ Lower labor demand.
√ Less tooling wear, roll forming doesn't create tool wear that press brake does.
√ Better dimensional control, due to the nature of roll forming itself, it tends to produce consistent dimension than other means of metal forming processes.

Ezen előnyök miatt a hengeralakítást széles körben alkalmazzák széles ipari alkalmazásokban, mint például ajtó ablakok, ereszcsatornák és házburkolatok, fiókcsúszkák, acél tartókeret, fémcsövek, korlátok, kerítésoszlopok, korlátrendszerek és napenergia. Amint látható, a hengeralakítás egyfajta fémalakítási folyamat, amelyet térfogat vezérel, ezért csak viszonylag nagyobb mennyiségû projektekhez alkalmas. A kis megrendelések drágábbak a fékformázáshoz képest a szerszámköltség és az egyéb üzemeltetési költségek, például a szerszámbeállítás és a próbaüzem miatt. Az alábbiakban összefoglaljuk a hengeralakítás hátrányait.
√ More expensive to produce compared to brake forming for small orders
√ Tooling is more expensive
√ The cost of equipment itself is usually higher than press brake
√ Requires bigger space
√ Tooling set up need to be done by an experienced operator, and tooling setup takes longer time
than press bending
√ More likely to produce end flare than brake forming due to linear stress
Fabmann can supply both simple and complex metal profiles made by press brakes and roll forming equipment, and we are using primarily stainless steel (304 and 316, 316L), CRC, HRC (Q235 equivalent to S235 or Q355 equivalent to S355), pre-galvanized coil like DX51D Z275, Z300 up to Z600 (single size zinc coating is above 42μm) according to EN 10327. We can produce complex steel profiles with holes punched online, and we also provide powder coating or hot dip galvanization according to your project requirement. Furthermore, we also design packing solution to make sure that your metal profiles will be fully protected throughout the whole transportation from China to your warehouse.